Food
Case packing, palletizing, and integrated packaging lines for snack bags, grain pouches, frozen food, and bakery products. Engineered for soft packaging that requires gentle handling and stable secondary transport.
Tailored packing solutions for diverse industries worldwide.
Case packing, palletizing, and integrated packaging lines for snack bags, grain pouches, frozen food, and bakery products. Engineered for soft packaging that requires gentle handling and stable secondary transport.
Case packing, palletizing, and integrated packaging lines for plastic bottles, glass bottles, beverage cans, and carton-packed beverage products. Engineered for high-speed production lines with stable stacking requirements.
Case packing, palletizing, and integrated packaging lines for milk cartons, yogurt cups, cheese packs, butter boxes, and other cold-chain dairy products. Built for hygiene compliance and stable carton loading.
GMP-oriented case packing, palletizing, and integrated packaging lines for pharmaceutical cartons, medicine bottles, medical devices, and diagnostic kits. Supports serialization, track-and-trace, and validation requirements.
Integrated pouch packing, bottle case packing, and palletizing lines for protein powder, collagen granules, capsule bottles, and nutraceutical blends. Engineered for premium retail packaging and stable secondary transport.
Case packing, palletizing, and integrated packaging lines for detergent pouches, cosmetic cartons, shampoo bottles, and personal care products. Engineered for high-speed production and reliable secondary packaging.
Turnkey secondary packaging automation engineered for continuous high-speed industrial plants.
View All Systems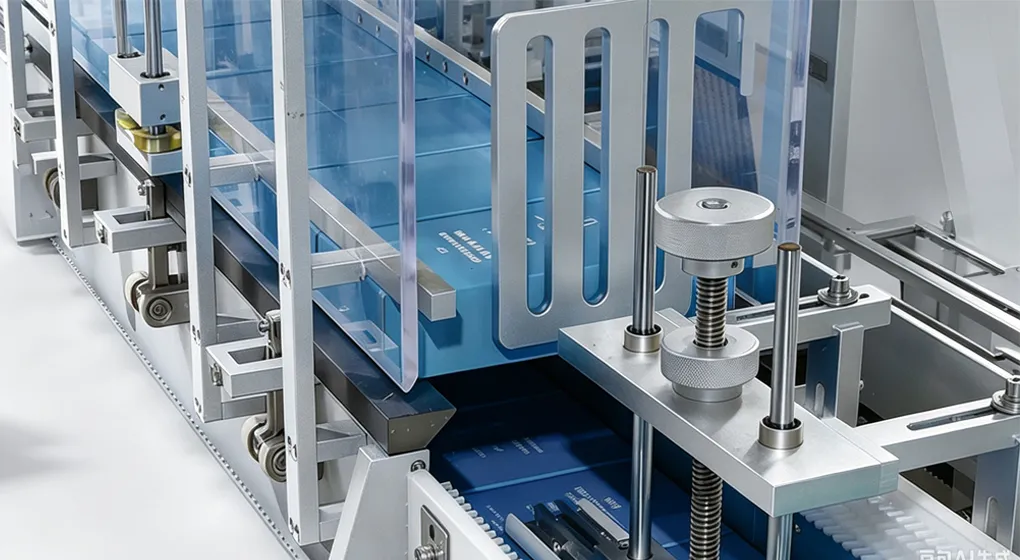
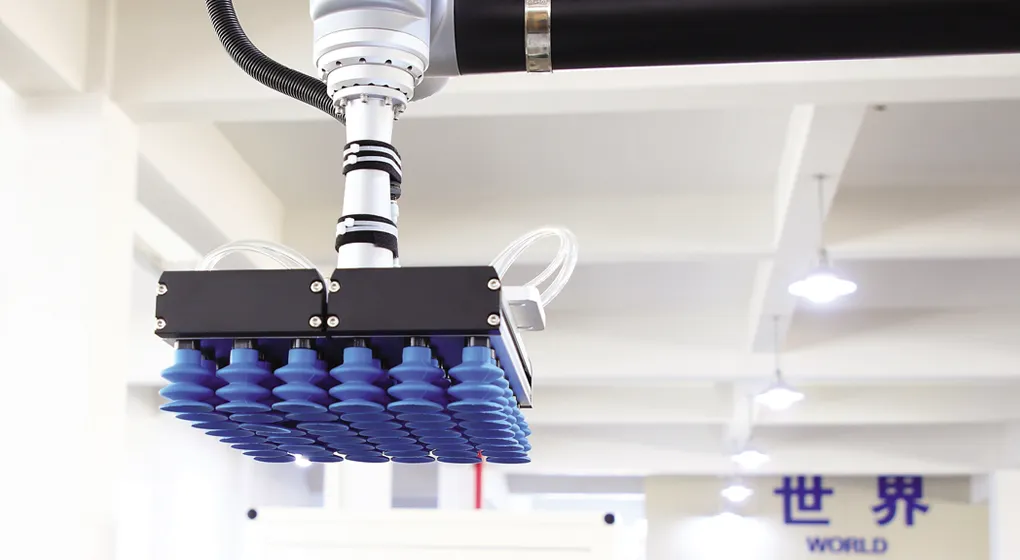
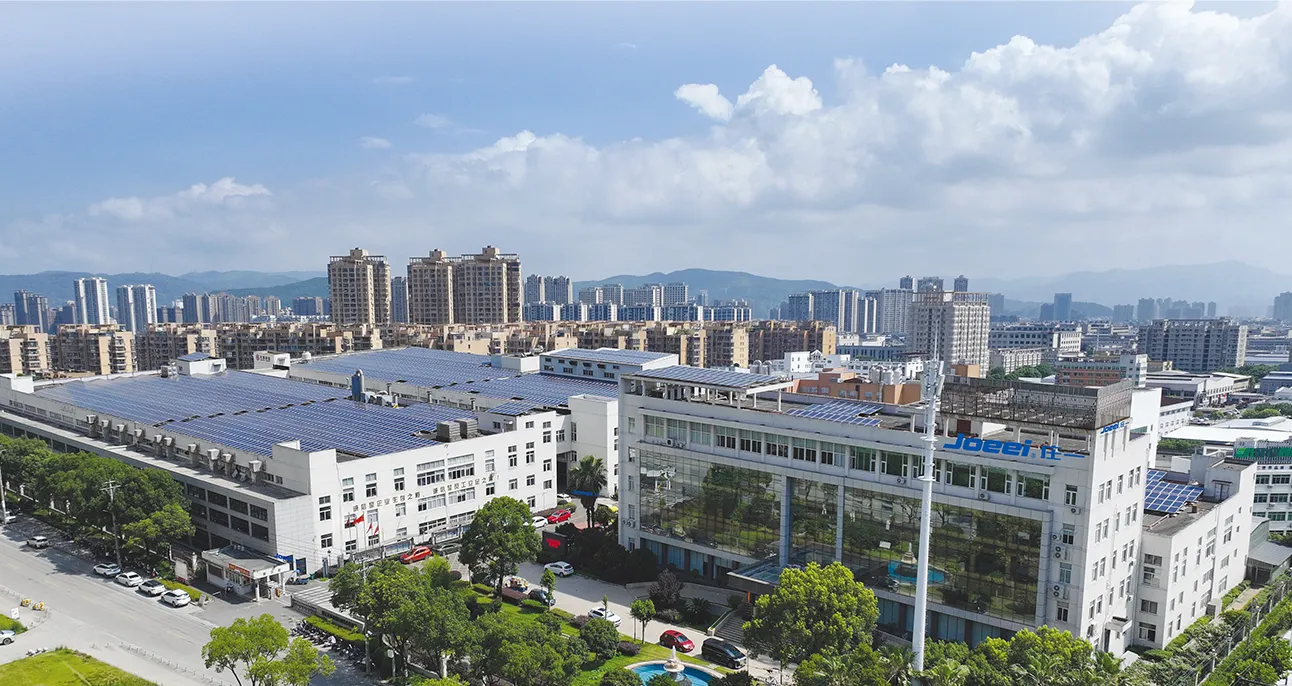
Founded in 2005, Joeei® has grown into a leading manufacturer of case packing and palletizing systems, serving over 30 countries with reliable, certified equipment.
More About Us
From industry trends to technical guides, sharing our observations and practices in case packing automation.
All ArticlesAutomatic case packers are high-potential packaging machinery widely adopted across food, beverage, pharmaceutical, and daily chemical industries. With continuous technological upgrades, modern case packing equipment achieves higher automation, precision, and intelligence to meet evolving factory production demands.
Automatic case packers deliver reliable performance for bottling packaging lines. This article lists five core equipment advantages from the manufacturer’s perspective and walks you through the full standard operating workflow for daily production.
Automatic case packers are deployed across many industries. Before putting the machine into formal operation, operators need to master critical usage notes, especially the technical specifications for incoming carton blanks, to avoid production failures during automated packing.
Modern automatic packaging machinery has become core equipment for manufacturing enterprise upgrading. As professional case packer manufacturers explain, intelligent packaging equipment greatly reduces production costs, improves operational efficiency, and realizes unmanned and standardized packaging workflows for long-term enterprise development.
Direct answers to engineering, lead time, and sample testing protocols.
We manufacture full-range secondary packaging machinery including top-load pick-and-place case packers, wrap-around cartoners, drop packers, robotic delta/articulated packing cells, and customized automated end-of-line packaging systems built to your product geometry.
As a direct machinery manufacturer, our MOQ is 1 unit for all standard and bespoke packaging lines. We support engineering trials and pilot plants, offering modular expansion capabilities as your production throughput scales.
Standard case packers typically ship within 25 to 35 working days. Tailored lines with bespoke robotics or multi-format infeed merges range between 35 and 50 days, strictly verified through complete in-house FAT running trials prior to dispatch.
Yes, physical sample testing is a mandatory step in our engineering protocol. You can ship product samples and corrugated carton blanks to our testing lab to confirm achievable packing speed, gripper suction reliability, and continuous line stability before full-scale build.
Engineering response within 24 hours guaranteed.